Category
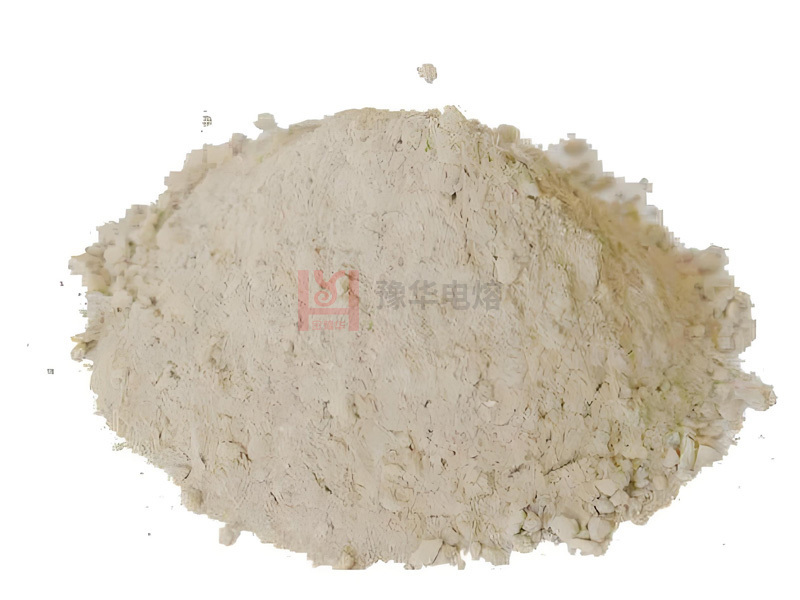

Zircon Mending Material
Classification:
Product Introduction
Product Details
Production method:
Zircon hot supplement: good high temperature resistance, refractoriness, load softening temperature and high temperature creep resistance and other indicators are close to the original brick, and has the corrosion resistance of glass and dust. Its main component is zircon sand as aggregate, with a small amount of alumina mixture; after sintering, the product is dense and the porosity is low. And has the characteristics of thermal shock resistance and high temperature volume stability. Therefore, thermal repair at high temperature does not produce cracking, chipping and other phenomena. Mainly used for the glass furnace hot repair; heat supplement in case of high temperature immediately after hardening, and can be firmly bonded with the original brick masonry, forming a whole structure, for the glass furnace hot repair to create excellent conditions and efficiency.
Method of use:
1. Adhesive preparation
The adhesive is aluminum dihydrogen phosphate, already prepared and packed in plastic bags. The rammed mixture shall be packed in polythene bags of 25kg each.
2. Mixing and stirring
A) Put aluminum dihydrogen phosphate in enough water for attenuation (metal containers should be avoided), then mix it with the tamped mixture, and mix it with a machine or manually.
B) Place the mixture for about 10 hours or longer for mixing and aging.
C) Judge whether the mixture is suitable for use. If it is too dry, add water and stir until it is suitable for use.
3. Construction
A) The construction site should be cleaned to avoid any impurities, and air hammer or manual compaction can be used.
B) The ramming movement shall be carried out in one direction without rest. Each ramming surface should cover another 1/3 of the area, and each layer of material should also cover another layer to avoid ignoring the space.
C) The thickness of the base mixture is 40-60mm, which shall be compacted to 1/2 of the thickness of the base after compaction. The surface of the compacted mixture shall be kept rough for the next compaction process to be continued until the required thickness of the mixture is achieved.
D) After the compaction process starts, it should be stopped immediately. If stopping cannot be avoided, the surface of the mixture should be kept rough and covered with plastic film to avoid delamination and induration.
E) When the entire process is completed
Physical and chemical indicators:
Indicators | Zroon | Al₂O | Fe2O3 | Unit Weight | Maximum Granularity | Moisty | Normal Temperature Compressive Strength | Firing Shrinkage % | Use Temperature |
ZSR-60 Zircon Ramming Compound | 60±2 | 4-7 | 0.5 | 3.40 | 4 | 3-5 | 45 | -1 | 400-1600 |
AZSC-30 Fused AZS Pouring Material | 29±1 | 47 | 0.5 | 3.00 | 5 | 6-8 | 75 | -1.2 | 100-1500 |
AZSS-40AZS-40 Sealing Compound | 40±2 | 38±2 | 0.5 | 2.90 | 1 | 3-5 | 50 | -1 | 100-1500 |
Keywords:
Zircon Mending Material
Kiln Display
Feedback
Leave an online message and get free product quotes
CONTACT US
WhatsApp:
E-mail:
Tel :
Address:
The Industry Park, XinMi City, Henan Province